Tool Grade Selection Guide: When Professional-Grade Pays Off (and When It Doesn't)
-
Why There's No Single Answer for Tool Specs
-
Scenario A: Air Ratchets Used Daily — Professional Grade Is Actually Cheaper
-
Scenario B: Occasional-Use, Big-Leverage Tools — Mid-Tier Is Enough
-
Scenario C: How Do You Dress a Diamond Grinding Wheel — Process Beats Tool Grade
-
Scenario D: Bosch Washers and Seals — Budget by Failure Consequence
-
How to Tell Which Scenario You're In
Why There's No Single Answer for Tool Specs
When a procurement colleague asks me "what grade should we spec for these tools," I always ask three questions back: How often will you use it? What happens when it fails? How tight is the precision requirement?
I'm not dodging. After nearly five years in a quality role—reviewing 200+ incoming deliveries a year—I've watched both failure modes play out. Someone buys professional-grade for a tool they'll use twice annually. Someone else saves a few dollars per unit on the cheap option and ends up paying ten times that in rework.
So I won't say "buy the expensive one" or "go budget." This piece breaks four common scenarios apart, each with a different answer.
The classification logic comes down to three variables:
- Usage frequency — daily use vs. a few times a year
- Failure consequence — just replace it vs. downtime and cascade damage
- Precision requirement — tolerance-controlled vs. "close enough works"
Jump to whichever scenario matches your situation.
Scenario A: Air Ratchets Used Daily — Professional Grade Is Actually Cheaper
Counterintuitive take first: for high-frequency tools, cheap usually costs more.
An air ratchet is the classic example. In an assembly bay or auto shop, one unit cycles hundreds of times a day. The failure mode on budget models isn't what happens out of the box — it's what happens around month three: the internal pawl wears and starts slipping, air seals degrade so torque drops to roughly 70% of rated output, and the reverse mechanism starts feeling vague.
We ran the numbers. A mid-tier air ratchet (~$90) needed replacement about every eight months. A professional-grade one ($180–250) ran two to three years. Over a three-year window, the mid-tier path meant buying four and a half units.
"The spreadsheet said go with the cheaper option—roughly 40% lower unit cost. My gut said no. Turned out the failure data we collected over 18 months proved the gut right: downtime on the cheaper units cost another $800 in delayed jobs."
Worth noting: the professional-grade advantage usually isn't peak torque—spec sheets look similar. It's the seal material, the heat treatment on the pawl, and the air port geometry. None of that shows up on a new unit. All of it shows up after several hundred hours.
One boundary to be clear about: I'm not a pneumatic tool design engineer, so I can't tell you which heat treatment suits which duty cycle. From a quality inspection angle, what I can tell you is how to make the decision based on long-run data.
Scenario B: Occasional-Use, Big-Leverage Tools — Mid-Tier Is Enough
Here's an opinion that runs against the usual advice: not every tool needs to jump to professional grade.
Take an 18 inch pipe wrench. If you use it fewer than ten times a year—occasional pipe repair at a facility or shop—mid-tier handles it fine. The design priority on this tool is bite force from the long handle, not precision.
I've seen more than one buyer upgrade pipe wrenches to professional grade just to "standardize the brand," paying more than double. What actually differs?
- Jaw hardness: professional grade wears slower after repeated bites on galvanized pipe, but with occasional use you won't feel the difference
- Handle material: professional uses forged aluminum, mid-tier uses cast iron with coating—lighter, but the weight difference is irrelevant at low frequency
- Tooth geometry: professional grade deforms thin-wall pipe less—this one matters if you regularly touch thin-wall stainless
Flip side: if you're using it several times a week, especially on thin-wall or deformation-sensitive pipe, the Scenario A logic applies—the professional-grade premium amortizes out over two years.
I hesitated on this call. The data suggested brand standardization would simplify procurement and reduce vendor management overhead. But when I ran the numbers, the added purchase cost far exceeded any process savings. So we split grades by usage frequency.
Scenario C: How Do You Dress a Diamond Grinding Wheel — Process Beats Tool Grade
I get this question a lot: how do you dress a diamond grinding wheel?
Start by separating two operations that get conflated. Dressing removes the dulled bond layer on the wheel surface to expose fresh diamond grit—restoring cutting ability. Truing restores the wheel's geometry and concentricity. Different methods, different frequencies.
Standard dressing approaches:
- Dressing stick: aluminum oxide or silicon carbide stick, fed manually or mechanically against the rotating wheel. Works for resin-bond and vitrified-bond diamond wheels. Feed rate stays small (typically 0.01–0.02mm per side per pass) and even.
- Diamond dresser: single-point or multi-point diamond tool for precision truing. This is for geometry, usually used alongside a dressing stick.
- Electrolytic dressing: common with metal-bond wheels; dissolves the bond electrochemically. This is a machine-level approach, typically on CNC grinders.
The most common mistake: dressing diamond with diamond. Logically it sounds right, but it's the wrong direction—using superabrasive to grind superabrasive damages both rather than producing a clean dress.
Second common issue is skipping coolant. Heat from dressing softens the bond or creates microcracks, particularly on resin bonds. If you see shiny spots on the wheel surface after dressing, that's usually a burned bond, not exposed grit.
"I assumed 'dressing' and 'truing' were the same thing. Didn't verify. Turned out I'd been dressing the wheel when I really needed to true it—two different operations, and I'd been doing the wrong one for three weeks."
Honestly, this crosses into grinding process engineering, which isn't my area. What I can tell you from a quality inspection perspective: if you're verifying dressing results, check two things—whether the surface has an even matte finish (exposed grit) and whether the workpiece surface roughness stays stable across test cuts. For specific dressing parameters, talk to a grinding process engineer or the wheel manufacturer's technical support.
Scenario D: Bosch Washers and Seals — Budget by Failure Consequence
Washers and seals look like the last parts worth thinking about, but failure consequences can be near the top of the list.
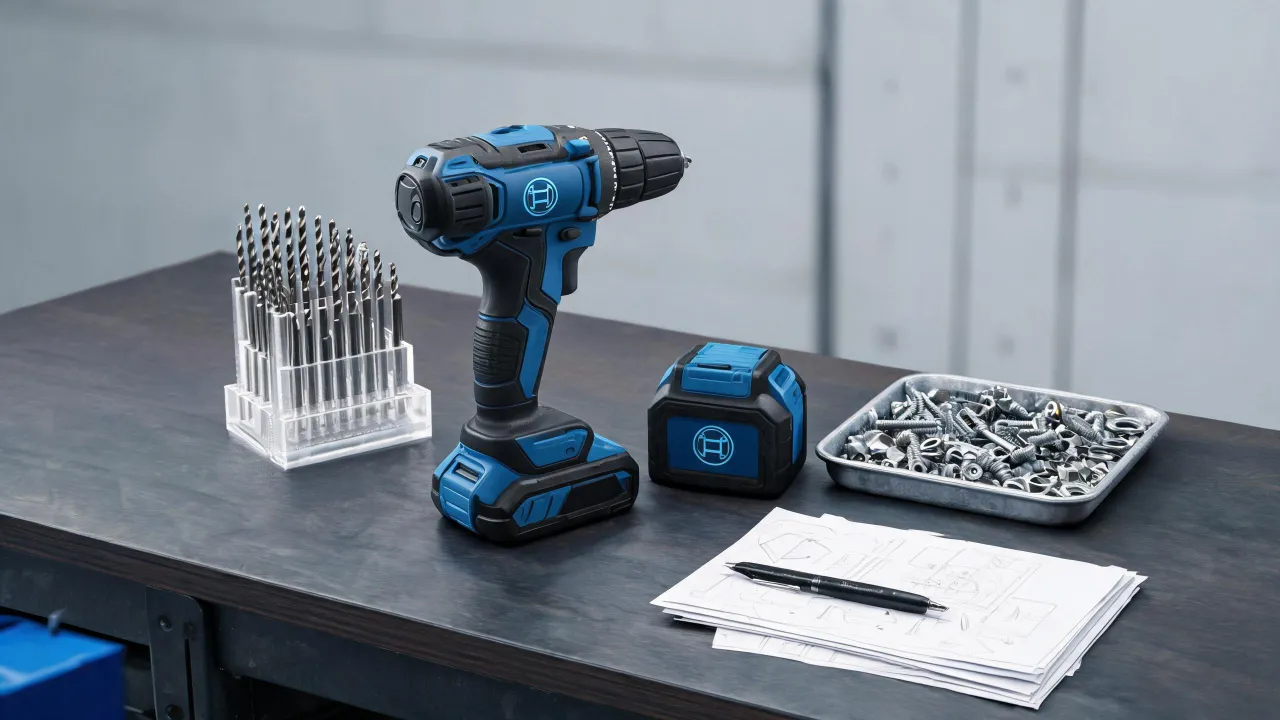
Bosch washers and seals show up widely in power tool maintenance—from gearbox seals to motor end-cap gaskets. The question: when replacing, use OEM or generic?
It depends on failure consequence. Two cases:
Case 1: failure means oil seepage or dust ingress, but core function is unaffected. Generic is fine here. Check three parameters—inner diameter, outer diameter, thickness—plus material compatibility (NBR vs. fluoroelastomer, depending on media contact and temperature).
Case 2: failure leads to motor water ingress, bearing burnout, or gearbox contamination. Use a Bosch washer here. Not because the OEM material is inherently superior—it's that the dimensional tolerance and installation geometry are validated matches. A 0.2mm compression difference can flip a seal from "sealing" to "weeping."
I made a classic error in my first year: assumed all washer spec standards were interchangeable. A batch of generic parts went in, looked fine short-term, and started weeping after three months. Turned out that batch's material hardness ran about 5 Shore A points low, which accelerated aging under our high-temperature duty cycle. That redo cost roughly $2,200 in teardown labor and replacement parts.
How to Tell Which Scenario You're In
A simple decision flow:
- Start with failure consequence. If a failure just means "replace it," you're in Scenario B or D Case 1. If it causes downtime, rework, or cascade damage, you're in Scenario A or D Case 2.
- Then check usage frequency. Weekly use usually amortizes the professional-grade premium. Less than monthly, mid-tier wins on value.
- Finally, check precision requirement. If you're controlling tolerance or surface finish (like Scenario C wheel dressing), consumable quality and process discipline matter more than the tool grade itself.
Here's the thing—most procurement mistakes aren't about buying the wrong grade. They're about jumping into price comparison before asking those three questions.
If you're unsure which scenario fits, pull the last three months of actual usage counts and failure records for that tool category. Data beats gut feel—though sometimes the gut is right too.
Helena Duarte
Helena Duarte is an independent pipe, valve, and pump applications analyst covering fittings, ball valves, gate valves, check valves, butterfly valves, flanges, hose clamps, centrifugal pumps, sump pumps, and submersible pumps. She uses ISO 5208 pressure-testing concepts and ISO 9906 pump acceptance methods while comparing pressure class, seat leakage, Cv, head, flow, efficiency, solids passage, seal materials, and installation orientation. Her guides help specifiers and maintenance teams match fluid-handling components to service conditions and acceptance criteria.